Mass calculator + engineering guide
316 Stainless Steel EOAT Bracket
Estimate plate mass and robot load, then check material, finish and interface requirements before requesting a quote.
Key decisions before specifying 316
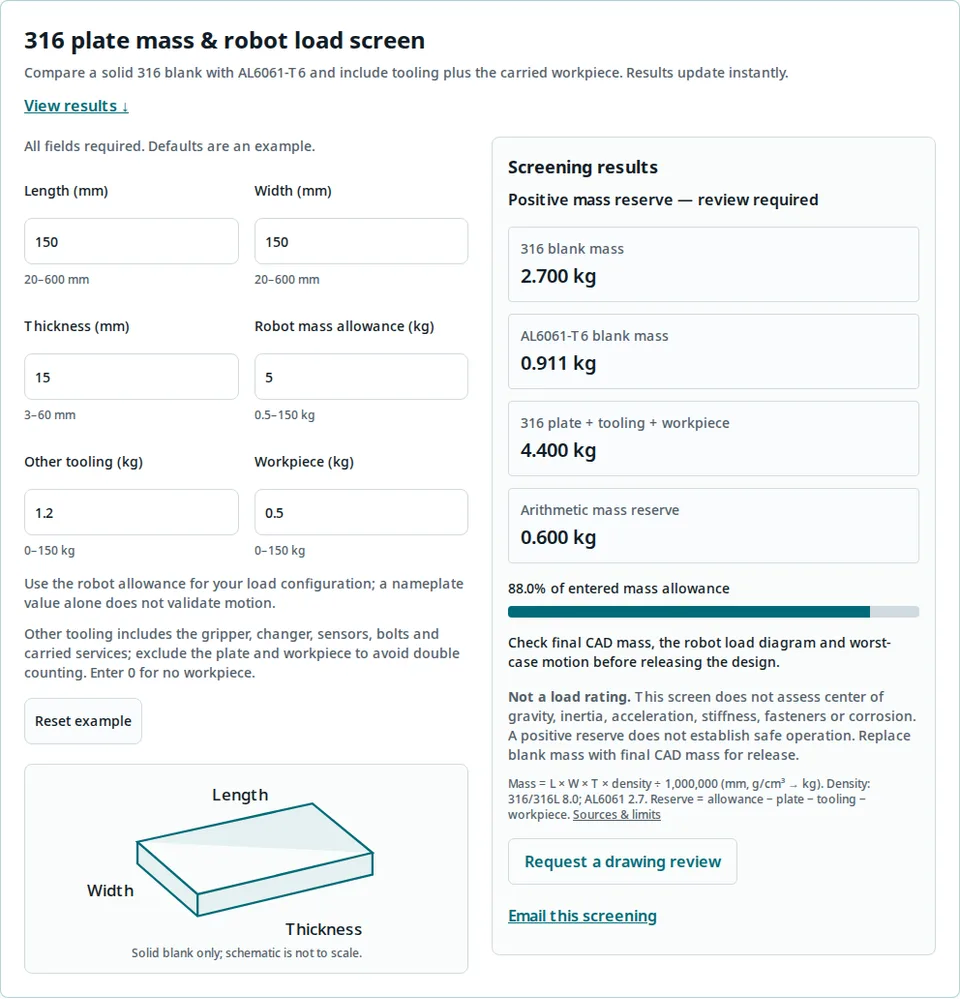
- Account for the full load and CoG offset: a 150 × 150 × 15 mm blank is 2.700 kg in 316 and about 0.911 kg in aluminum. Add tooling and the workpiece before comparing with the robot allowance. A heavy stainless bracket pushes the entire payload's center of gravity (CoG) further from the flange. You must verify this extended Z-offset against the manufacturer's Payload vs. CoG Offset curve to ensure the load remains in the safe zone, otherwise inertial forces during rapid moves will trigger protective stops. Calculation below.
- Separate corrosion from welding: 316 contains 2–3% molybdenum for chloride resistance; 316L limits carbon for welding-related concerns. Neither is immune to concentrated cleaning solutions. While peracetic acid (PAA) is generally safe at low concentrations,chlorides in washdown water can still cause severe pitting if allowed to pool and stagnate in crevices. Sodium hypochlorite (bleach) requires immediate rinsing with low-chloride water. Outokumpu data.
- Specify geometry and finish together: a roughness target alone does not establish cleanability or certification. Deep counterbores and tight sensor pockets create stagnation zones that defeat passivation and trap washdown chemicals. 3-A primer.
- Quote the actual process: work hardening and chip control affect stainless machining. 316 has an AISI machinability rating of ~60 (vs ~70 for 304). The added molybdenum makes it "gummier," requiring slower cutting speeds and increasing tool wear. Expect raw material and processing costs for a 316 bracket to be 20–40% higher than 304. Sandvik material guidance.
Method: blank mass first, assembly validation next
For dimensions in mm and density in g/cm³: mass (kg) = length × width × thickness × density ÷ 1,000,000. The 316 and 316L screening density is 8.0; the aluminum comparison uses 2.7. The same geometry has a mass ratio of 8.0 ÷ 2.7 ≈ 2.96.
Arithmetic reserve = entered robot mass allowance − blank mass − other tooling − workpiece. There is no assumed 80% safety threshold. The supported input ranges limit this estimator, not the factory's machining capability.
1. Screen
Enter dimensions and complete carried mass.
2. Validate
Check chemistry, final CAD mass and robot load envelope.
3. Specify
Release interface, finish and inspection requirements.
| Scenario and assumptions | Calculation | Result and next step |
|---|---|---|
| 5 kg allowance; default blank; 1.2 kg tooling; 0.5 kg part | 5 − 2.700 − 1.200 − 0.500 | 0.600 kg reserve. Check center of gravity, inertia and motion. |
| Same assembly; carried part rises to 1.2 kg | 5 − 2.700 − 1.200 − 1.200 | −0.100 kg reserve. Revise mass or robot selection. |
| Same 5 kg configuration with aluminum; 0.5 kg part | 5 − 0.911 − 1.200 − 0.500 (rounded) | About 2.389 kg reserve. Verify aluminum compatibility and stiffness before substitution. |
316 stainless steel vs AL6061-T6
Compare equal blank geometry first. Material choice still needs a separate load-path and exposure review; weight does not establish strength.
| Decision factor | 316 / 316L | AL6061-T6 |
|---|---|---|
| Density used | 8.0 g/cm³, nominal at 20°C. Physical properties, p. 8 | 2.7 g/cm³, rounded from 0.098 lb/in³. Hydro, p. 2 |
| 150 × 150 × 15 mm solid blank | 2.700 kg | 0.911 kg (rounded) |
| Exposure decision | Review the actual cleaner and crevice conditions. | Review base metal, coating compatibility and wear. |
| Machining plan | Plan for aggressive work hardening and heat generation. Cutting speeds are substantially lower (often 60–100 m/min). | Highly machinable, allowing faster feeds and speeds with excellent chip evacuation. |
| Strength and stiffness | Obtain product-form and condition-specific properties; check plate and joint stresses. | Verify temper, deflection and thread engagement; do not substitute solely by mass. |
| Price and lead time | Higher material cost, faster tool wear, and longer cycle times drive up unit price (often 2-3x the cost of aluminum). | Generally the most cost-effective baseline due to high machinability and lower raw material cost. |
316 vs 304 — and what 316L changes
Molybdenum improves localized corrosion resistance; lower carbon addresses welding-related sensitization. The Outokumpu datasheet, pp. 2–4 also describes conditions where higher-alloyed grades may be needed.
| Question | Useful distinction | Action before release |
|---|---|---|
| Mild cleaning or dry automation? | 304 may meet the exposure requirement; 316 is not automatically necessary. | Review the plant material specification and actual cleaning process. |
| 316 or 316L for a welded assembly? | 316L reduces sensitization risk after welding; it is not a universal chloride upgrade. | State the required grade and weld/post-treatment procedure. |
| Bleach, brine, marine splash or hot crevices? | Both 316 and 316L can suffer localized corrosion. | Obtain compatibility evidence; evaluate higher alloys or redesign when needed. |
| Can PREN alone approve a plate? | PREN is a composition-based comparison, not a service-life guarantee. | Do not apply a universal seawater threshold or ignore temperature and geometry. |
| Are 304 and 316 structurally interchangeable? | Grade names alone do not specify allowable stress or joint stiffness. | Check stock condition, material certificate and application loads. |
| Does 316 cost more to machine than 304? | Yes. 316 has an AISI machinability rating of ~60 vs 304's ~70. The molybdenum content makes it gummier, increasing tool wear and cycle time. | Expect a 20–40% combined material and machining cost premium for 316. Only specify 316 if the exposure requires it. |
Choose a material for the use condition
The following are screening recommendations, not compatibility approvals.
| Use condition | Candidate direction | Confirm before ordering |
|---|---|---|
| Dry, payload-sensitive tooling | Evaluate AL6061-T6; consider 304 if stainless is specified. | Coating, wear, stiffness and the customer material rule. |
| Washdown with defined cleaning chemistry | Evaluate 316 against documented exposure. Peracetic acid (PAA) is generally safe; Sodium Hypochlorite (Bleach) risks pitting if >20 ppm or not rinsed. | Concentration, temperature, contact time, rinse protocol, and drainage. |
| Welded stainless adapter assembly | Evaluate 316L and the weld process together. | Grade traceability, weld treatment and finished surface condition. |
| Aggressive chloride exposure | Request a corrosion review; a higher alloy may be needed. | Service evidence or representative exposure testing. |
| High acceleration or long tool overhang | Review a lighter geometry or material if permitted. | Robot load envelope, inertia, stiffness and accessible cleanable pockets. |
Interface, finish and inspection requirements
| Interface or feature | Specify | Requested evidence |
|---|---|---|
| Robot-side and tool-side faces | Separate bolt circles, pilot diameters, dowel locations, datums and clocking. | Inspection results for mating and locating features. |
| Fasteners and inserts | Thread form, engagement, class, counterbore depth and access. | Assembly review with the mating drawings; avoid a generic torque assumption. |
| Surface finish | Ra, measurement locations and applicable contact zone; 0.8 µm (about 32 µin) only where required for IP69K or hygienic washdown. | Roughness results for called-out surfaces. Eliminate internal crevices where possible. |
| Passivation | Specify the method: "Citric 2" (eco-friendly, preserves tolerances) or "Nitric 1" (aggressive, legacy specs) per ASTM A967. | Process record and agreed acceptance evidence (e.g., copper sulfate test). |
| Material and traceability | 316 or 316L, stock form/condition, drawing revision and required certificate. | Material certificate tied to the supplied part or lot. |
The 3-A primer discusses product-contact finish and cleanability. ASTM A967/A967M-25 covers passivation methods and alternative verification tests; the selected process does not establish suitability for every application.
Design risks and practical mitigations
| Risk | Consequence | Mitigation or alternative |
|---|---|---|
| Missing workpiece or changer mass | The assembly can exceed the robot allowance. | Use the heaviest part; inventory all carried components and weigh the assembly. |
| Positive mass reserve treated as approval | Overhang, inertia or acceleration can exceed robot limits. | Check the manufacturer load diagram and motion setup for the specific robot. |
| Wrong exposure assumption | Pitting, crevice corrosion or shortened service life. | Confirm cleaner details, eliminate traps and obtain material compatibility evidence. |
| Pocketing solely to save mass | Lost stiffness or inaccessible cleaning cavities. | Review structural load paths and cleanability together; consider another material where allowed. |
| Unquoted finishing and inspection | Late price changes or disputed acceptance. | Quote drawing revision, process sequence and inspection requirements as explicit line items. |
| Mating pattern or datum mismatch | Dowels, bolts or pilots do not assemble correctly. | Review both interface drawings; inspect critical locations before finishing or final shipment as appropriate. |
Key engineering conclusions
- Mass penalty and CoG offset: 316 stainless is nearly 3× heavier than aluminum. For complex EOAT assemblies, this extra mass pushes the Total Flange Load and Center of Gravity (CoG) offset further from the wrist. This creates a lever-arm effect that drastically increases moment loads (torque) on joints J4–J6. Always evaluate the extended Z-offset against the manufacturer's dynamic load curve (e.g., UR15 payload derating curves), as inertial forces during rapid moves will trigger protective stops even if the absolute mass is below the static maximum.
- Corrosion vs. cost: 316/316L resists chloride pitting better than 304, making it mandatory for harsh washdown (e.g., meat processing, medical). However, the ~60 machinability rating of 316 (compared to ~70 for 304) means cutting speeds must be reduced to 60–100 m/min to manage work-hardening and tool wear, generally resulting in a 20–40% higher final part cost compared to 304. Furthermore, 316 is not invincible—it can still pit if exposed to concentrated sodium hypochlorite (bleach) for extended periods without rinsing, or if PAA is contaminated with chlorides and allowed to stagnate in crevices.
- EOAT routing: Unlike simple end effectors, complete EOATs often require pneumatic and electrical routing. If the bracket includes pass-throughs, internal crevices must be designed for cleanability, especially when using sanitizers like peracetic acid (PAA) which demand fully drainable geometry.
- Interface stiffness: Heavy stainless plates can induce vibration if the interface bolt pattern is narrow relative to the plate size. Dowel pins are critical for repeatability.
Evidence, standards and limits
Published by EOAT Machining on . Last reviewed .
Sources checked . Nominal material data support screening. Supplier prices, lead times, corrosion life and assembly load capacity remain unknown until the drawing and application are reviewed.
| Source | What it supports | Limit of use |
|---|---|---|
| Outokumpu Supra datasheet (PDF) | 316/316L nominal density (p. 8); corrosion and welding distinctions (pp. 2–4). | Use actual stock properties and exposure details for release. |
| Hydro Alloy 6061 (PDF) | Density 0.098 lb/in³ (p. 2); rounded here to 2.7 g/cm³. | Extruded product data; strength values must match the purchased plate/stock and temper. |
| Sandvik workpiece materials | Austenitic stainless work hardening, chip formation and cutting challenges. | General AISI ratings (60 for 316, 70 for 304) reflect baseline difficulty, but exact tool life and cycle time depend on geometry. |
| ASTM A967/A967M-25 | Scope of chemical passivation: both Nitric (aggressive) and Citric (eco-friendly, preferred for tight tolerances) are approved. | Specify the exact method (e.g., "Citric 2"). The standard alone does not guarantee performance without acceptance testing. |
| 3-A sanitary-design primer | Cleanability, contact zones and generally 32 µin Ra or smoother product-contact surfaces. | Introductory guidance; confirm the specific equipment standard and customer requirement. |
| Sanitation guidelines (Industry standard) | Peracetic acid (PAA) is generally safe, but chlorides in washdown water or pooling in crevices drastically accelerates pitting. | Exact corrosion resistance requires application-specific testing of the total water chemistry. |
| Universal Robots UR15 manual, SW5.24 | Payload vs. CoG Offset curves. The allowable payload decreases as the CoG extends further from the tool flange. | Illustrates why the "lever arm" from a heavy bracket necessitates payload derating. Use the manual for your specific robot model. |
RFQ checklist: make the quotation reviewable
- STEP model plus a revision-controlled drawing; identify the robot-side and tool-side interfaces.
- Robot model and load diagram, complete tooling mass, maximum workpiece mass and motion profile.
- Specified 316/316L grade, stock condition and required material certificate.
- Cleaner chemistry, concentration, temperature, contact time and product-contact zone.
- Finish, edge breaks, passivation treatment, datum tolerances and inspection evidence.
- Quantity, delivery destination and requested schedule. Agree confidentiality terms before transferring sensitive drawings.
Continue with our materials overview, quality process or machining capabilities for supplier review.
Review the robot flange and bracket product family for interface scope, compare the 304 stainless bracket guide for milder exposure, or request confidentiality terms for CAD transfer.
Frequently asked questions
Material & cleaning
Why choose 316 instead of 304?
Consider 316 where the specified exposure calls for molybdenum-bearing stainless. Confirm the actual cleaner, concentration, temperature and crevice conditions before selecting the grade; neither grade is immune to corrosion.
Is 316L more resistant to chlorides than 316?
The L designation specifies lower carbon and is principally useful for limiting sensitization associated with welding. It is not a general chloride-resistance upgrade. Ask for an exposure-specific material review.
Is 316 required for every food or medical robot?
No. Product-contact zone, cleaning procedure and the applicable customer specification determine the material and finish. Grade selection alone does not establish hygienic compliance.
Does passivation replace polishing?
No. Define the required roughness separately, then specify cleaning, passivation treatment and acceptance testing. Passivation does not remove an unsuitable crevice or correct a rough machined surface.
Calculator & robot integration
How accurate is this mass estimate?
It calculates a solid rectangular blank using nominal density. It does not deduct holes or pockets and does not add inserts. Compare the finished CAD mass with an actual weighed assembly before release.
Does a positive reserve mean the adapter is safe?
No. It only means entered masses sum to less than the entered robot allowance. Check the robot load diagram, center of gravity, inertia, motion profile, plate stiffness and fastener loads separately.
Where should I enter the carried part?
Use the Workpiece field. Other tooling covers the gripper, changer, fasteners, sensors and carried services, excluding the plate and workpiece. Use the heaviest production part.
What if my dimensions are outside the supported range?
The tool covers 20–600 mm length and width, 3–60 mm thickness and 0.5–150 kg robot allowance. These are estimator limits. Send CAD and your robot data for a manual review.
Drawing & procurement
What tolerances should I specify?
Dimension the robot-side and tool-side bolt patterns from explicit datums. Call out pilot fits, locating dowels, face flatness and perpendicularity only where they control the interface. Use the mating component drawings.
Can pocketing reduce the weight?
Yes, but the saving is geometry-dependent. Review local stiffness, remaining wall thickness, tool access, fastener engagement and drainage before accepting a pocketed design. The calculator does not predict the saving.
How much more does 316 cost?
A universal percentage is not reliable. Obtain dated quotes for identical CAD, quantity, stock form, tolerances, finish, inspection and delivery terms; compare material and processing costs separately.
What should I send for a quote?
Send STEP and a revision-controlled drawing, robot and mating-interface drawings, tooling/workpiece masses, quantity, cleaner details, finish and passivation requirements, inspection needs and delivery destination.
Request a 316 bracket drawing review
Send the RFQ inputs above for material, interface and manufacturing review. Use “Email this screening” in the calculator to include the current inputs and results.
Open the inquiry formInquiry Email
Attach your CAD files (STEP, IGES) and tolerances for quick quoting.